Home › Silicone Rubber › Pad Printing Silicone
Pad Printing Silicone Rubber Built for Clear, Repeatable Transfer
Two-component RTV-2 silicone rubber for manufacturing durable printing pads. Choose platinum-cure PPA for low shrinkage and dimensional stability, or tin-cure PPC for a practical, conformable pad-making system.
Start with the Part. Then Choose the Pad.
Share the print area, part geometry, ink and solvent, required pad hardness, production rhythm and current failure mode.
Choose by Process Priorities, Not by Hardness Alone.
Pad shape, wall thickness, compression, artwork, substrate geometry, ink, solvent and silicone-oil addition all influence print performance.
CREKEM PPA and PPC are liquid silicone systems for making silicone printing pads. The finished pad picks up ink from the cliché and transfers it onto flat, curved or irregular parts. This combined range keeps the selection path clear while still giving each chemistry the technical detail it needs.
PPA Addition Cure Pad Printing Silicone
9:1 by weight≤0.1% shrinkage- Low shrinkage for stable pad geometry
- Rapid elastic recovery and repeatable transfer
- Shore A 15, 20 and 30 development grades
- Best when dimensional consistency is the priority
PPC Condensation Cure Pad Printing Silicone
100:3 by weight≤0.2% shrinkage- Fine-detail reproduction on irregular surfaces
- Balanced surface tack and elastic recovery
- Shore A 10, 15, 20 and 30 development grades
- Practical choice across general pad-making needs
Compare Every Grade in One Horizontal Matrix.
Scan the complete PPA and PPC range by row. The first column stays visible while you move across the technical properties.
| Product | Cure system | Hardness Shore A | Mix ratio A:B by weight | Mixed viscosity mPa·s at 25°C | Pot life / Cure at 25°C | Linear shrinkage | Mechanical properties |
|---|---|---|---|---|---|---|---|
| PPA15 | Addition cure | 15 ± 2 | 9:1 | 12,000 ± 2,000 | 30–60 min 3–6 h | ≤0.1% | Tear ≥18 kN/m Tensile ≥6 MPa Elongation ≥450% |
| PPA20 | Addition cure | 20 ± 2 | 9:1 | 15,000 ± 2,000 | 30–60 min 3–6 h | ≤0.1% | Tear ≥25 kN/m Tensile ≥6.8 MPa Elongation ≥560% |
| PPA30 | Addition cure | 30 ± 2 | 9:1 | 16,000 ± 2,000 | 30–60 min 3–6 h | ≤0.1% | Tear ≥25 kN/m Tensile ≥7 MPa Elongation ≥550% |
| PPC10 | Condensation cure | 10 ± 2 | 100:3 | 18,000 ± 2,000 | 30–40 min 3–5 h | ≤0.2% | Tear ≥10 kN/m Tensile ≥3 MPa Elongation ≥350% |
| PPC15 | Condensation cure | 15 ± 2 | 100:3 | 20,000 ± 2,000 | 30–40 min 3–5 h | ≤0.2% | Tear ≥12 kN/m Tensile ≥3.2 MPa Elongation ≥380% |
| PPC20 | Condensation cure | 20 ± 2 | 100:3 | 22,000 ± 2,000 | 30–40 min 3–5 h | ≤0.2% | Tear ≥15 kN/m Tensile ≥3.5 MPa Elongation ≥450% |
| PPC30 | Condensation cure | 30 ± 2 | 100:3 | 25,000 ± 2,000 | 30–40 min 3–5 h | ≤0.2% | Tear ≥18 kN/m Tensile ≥3.2 MPa Elongation ≥420% |
A Controlled Six-Step Pad-Making Process.
Bring materials, mold and tools to 23–25°C. Keep surfaces dry and contamination-free.
PPA: 9:1. PPC: 100:3. Weigh by mass unless the approved label states otherwise.
Mix thoroughly. Use only approved pigments, silicone oil or modifiers within a validated window.
Vacuum degas where possible, then pour slowly from one point into the pad mold.
Follow the grade-specific cure schedule before careful demolding and conditioning.
Check geometry, compression, image transfer, ink and solvent compatibility, and pad life.
One Flexible Pad. Many Difficult Surfaces.
Pad printing transfers graphics onto surfaces that are difficult to reach with direct printing. Silicone flexibility lets the pad conform while releasing ink onto the part.
Typical uses: electronics, keyboards, toys, automotive parts, appliances, promotional goods and molded plastic components.
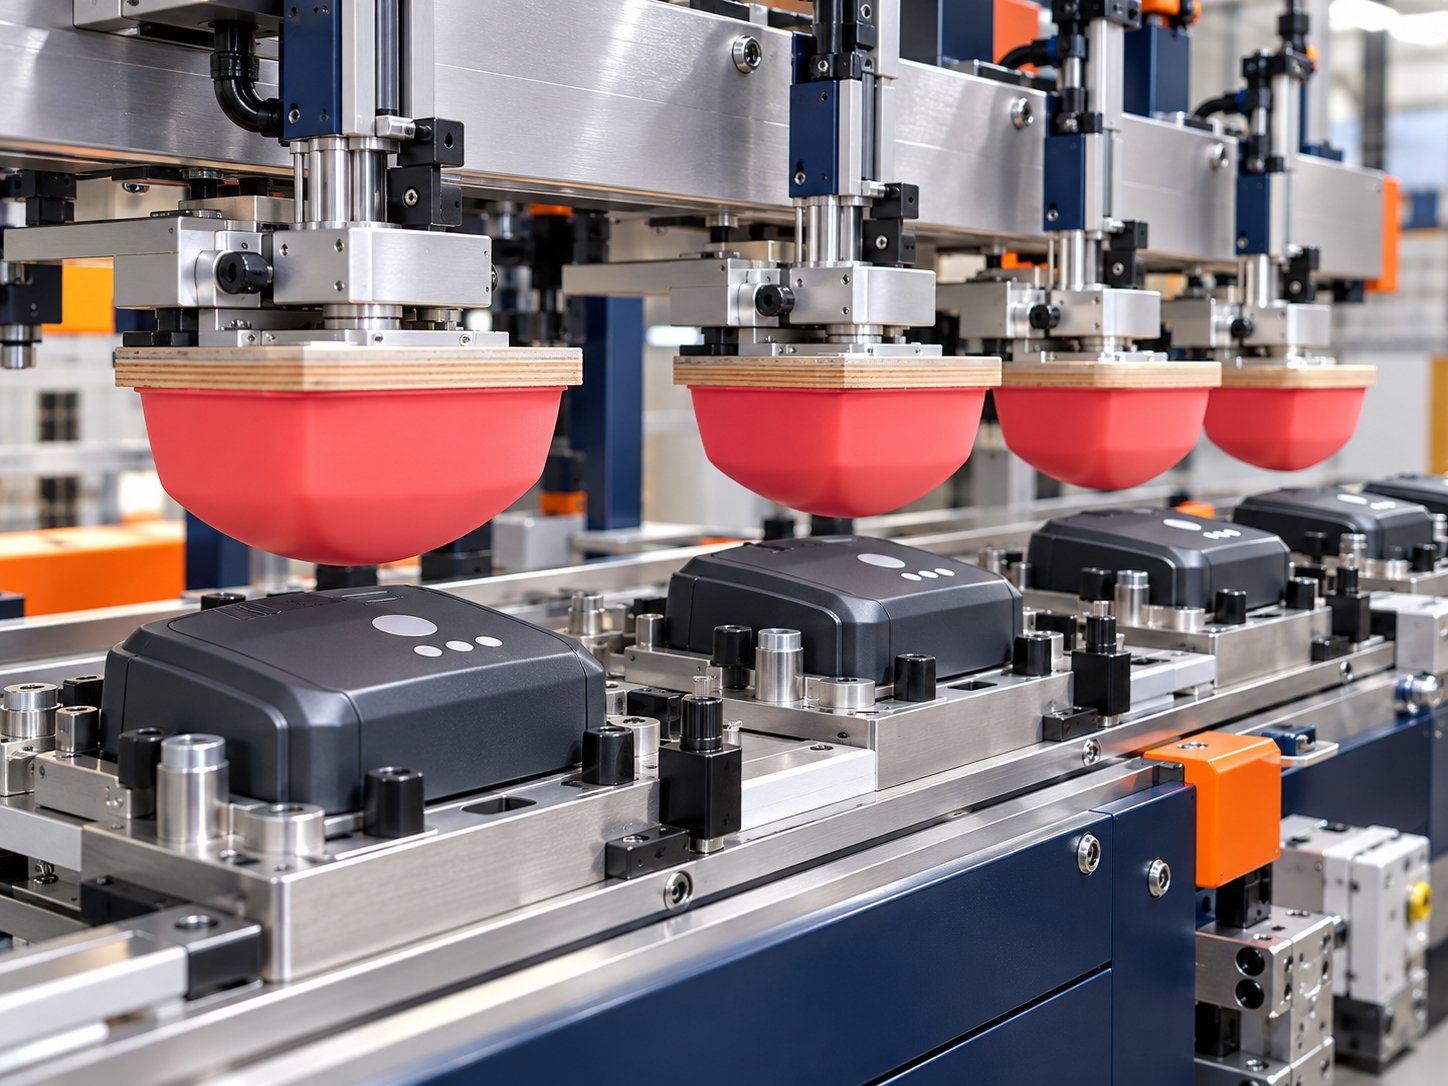
Automated Multi-Pad Production
Consistent pad recovery supports repeated transfer across multi-station industrial printing lines.
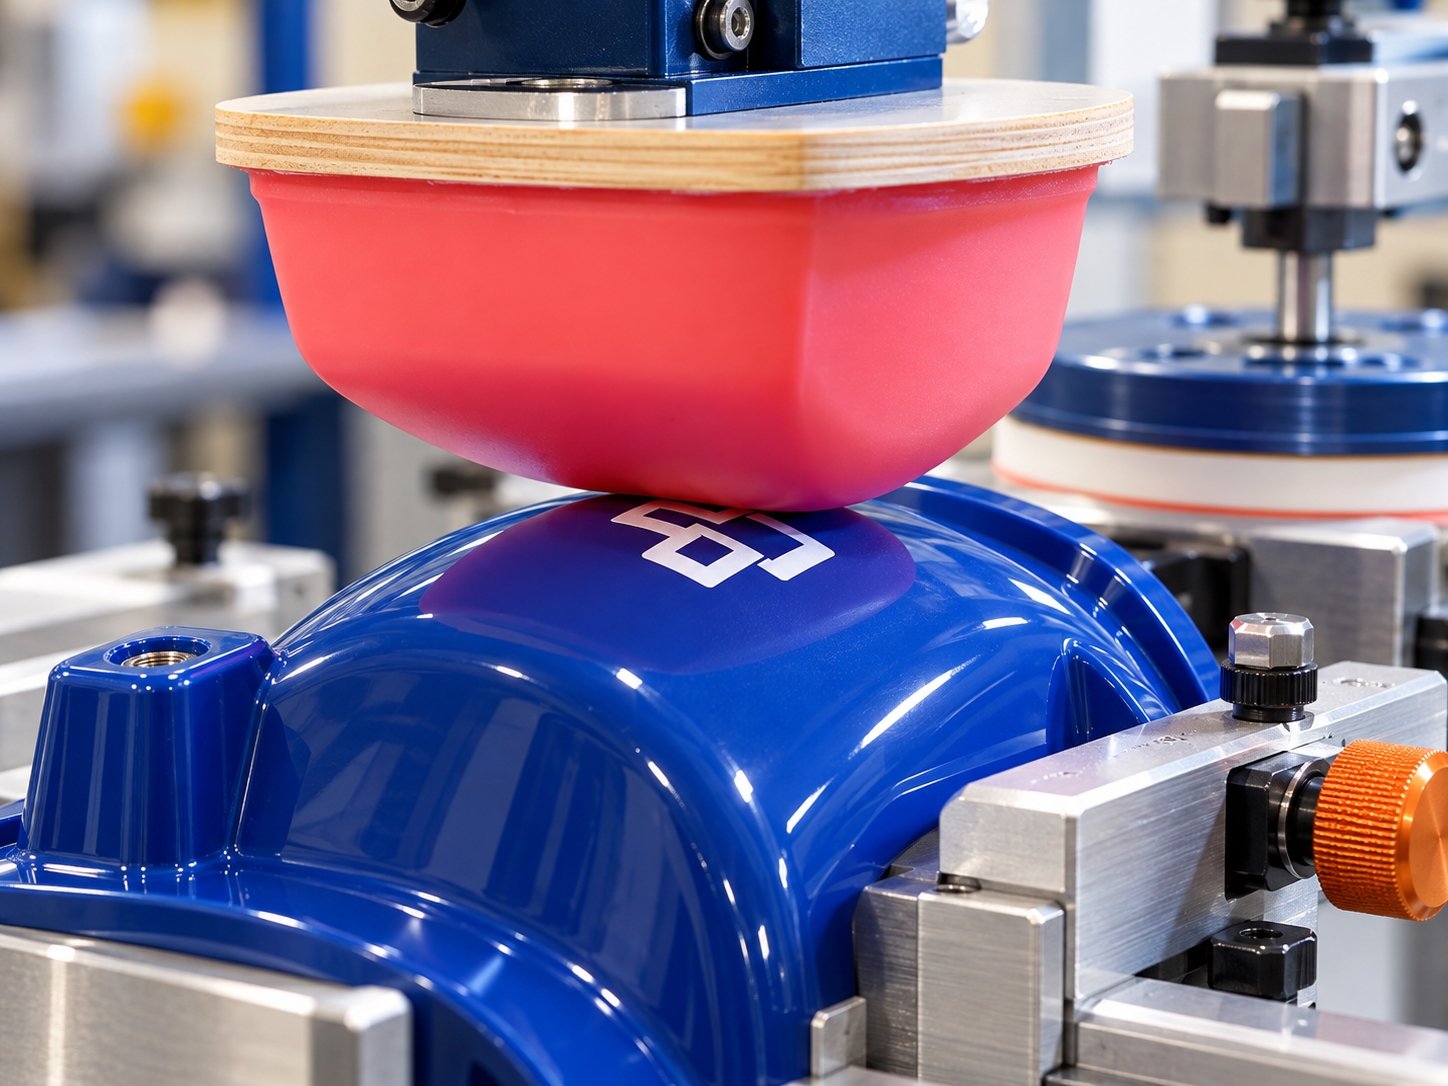
Precision on Molded Parts
A conformable silicone pad reaches curved and recessed areas while supporting controlled image transfer.
What Changes the Print?
Blurred edges or incomplete transfer
Review pad geometry, hardness, compression and ink release.
Inconsistent results on curved parts
Use a more conformable grade or adjust pad shape and contact pressure.
Premature pad wear
Evaluate tear resistance, solvent exposure, oil addition and production rhythm.
Keep the Two Chemistries Separate.
Platinum-cure PPA can be inhibited by sulfur-containing clays, amines, organotin residues, natural latex, some pigments and contaminated tools. Tin-cure PPC residues can also inhibit addition-cure silicone.
Use dedicated tools and work areas, and always run a compatibility test on the actual mold, pigment, silicone oil and other additives.
Technical Questions Buyers Ask First.
What is pad printing silicone rubber used for?
It is a two-component liquid silicone material used to mold flexible printing pads. The cured silicone pad picks up ink from a cliché and transfers the image to flat, curved or irregular parts.
Should I choose addition-cure or condensation-cure pad printing silicone?
Choose PPA addition cure when low shrinkage and dimensional stability are key priorities. Choose PPC condensation cure when you want a practical system with a broad Shore A 10–30 starting range. Confirm the final grade through a production trial.
What hardness is best for a silicone printing pad?
Softer grades conform more easily to deep contours and pronounced curvature. Harder grades generally support stable registration and clear graphics. Pad shape, wall thickness, compression and artwork must be evaluated together with hardness.
Can silicone oil be added to make the printing pad softer?
Approved silicone oil can be used within a validated formulation window. Excess oil may reduce strength, increase swelling or bleed, and shorten service life.
How do I prevent bubbles in a silicone pad?
Mix carefully, vacuum degas where possible, and pour slowly from one point. Clean, dry tools and a suitable mold design also help reduce trapped air.
Does CREKEM supply finished printing pads or pad printing machines?
This page covers liquid RTV-2 silicone rubber raw material for manufacturing printing pads, not finished pads, machines, clichés or printing inks.
Send the Part Details. We’ll Narrow the Grade.
Tell us your substrate, print area, pad shape, hardness target, ink and solvent, current issue, sample quantity and destination.